


Machine vision lighting is the LED illumination that lets an industrial camera see what you need to inspect: edges, surface defects, codes and outlines. VA Imaging Inc. supplies bar lights, ring lights, dome lights, coaxial lights, backlights, spot lights and line scan lights to US manufacturers, OEMs and system integrators, with every price shown in US dollars. Our team in Charlotte, North Carolina helps you choose the right light type, wavelength and power supply for your inspection setup. Compare ring lights for close-range inspection or bar lights for larger fields of view.


Machine vision lighting refers to specialized industrial lighting used to illuminate objects so a camera can capture clear images for automated analysis. In a machine vision system, lighting is not simply used to make an object visible. It is used to control how the camera sees the object.
A properly selected light can highlight edges, reveal surface defects, reduce glare, create silhouettes, improve contrast, and separate the target object from the background. This helps the vision system detect important details more accurately and consistently.
Machine vision lighting is widely used in applications such as automated inspection, product identification, dimensional measurement, defect detection, barcode reading, surface inspection, object recognition, placement verification, part alignment, and quality control on production lines.
LED Machine vision lights are commonly used because they provide stable illumination, long service life, efficient operation, and flexible configuration options. Depending on the application, lights can be selected in different colors, wavelengths, sizes, intensities, and form factors.
VA Imaging Inc. offers machine vision lighting solutions through an online store with quick delivery options. A selection of popular lights is also available from local express stock for fast shipping. For applications that require a specific size, wavelength, power output, or mechanical design, customization is available across many machine vision lighting series.
In automated inspection, poor lighting can lead to unreliable results. Even a high-quality industrial camera may struggle if the lighting produces reflections, shadows, uneven illumination, or low contrast. Vision software can only analyze what the camera captures, so stable and controlled Vision System Lighting is essential.
The right lighting helps improve image consistency, contrast between the object and background, defect detection, measurement accuracy, barcode readability, inspection repeatability, and overall machine vision performance.
Different objects require different lighting strategies. A reflective metal part may need
diffuse lighting to reduce glare. A transparent or semi-transparent object may
require back lighting to define its outline. A moving product on a conveyor may need line scan lighting for continuous inspection. A small component may require a ring light for close-range, even illumination.
Because every inspection environment is different, selecting the right machine vision
lighting requires careful consideration of the object, camera angle, surface texture, required contrast, working distance, and production conditions.
With our office in Charlotte, VA Imaging Inc. helps the US market source and implement machine vision lighting for industrial automation projects. We support customers looking for standard products as well as customized lighting solutions for specific inspection challenges.
US manufacturers often need lighting that can perform reliably in demanding production environments. Consistent output, accurate color rendering, long lifetime, and repeatable batch quality are all essential. VA Imaging Inc. focuses on helping customers select lighting solutions that support long-term machine vision performance.
Whether your application requires LED Machine vision lights for a new production line, replacement lighting for an existing inspection system, or custom Vision System Lighting for a specialized machine, VA Imaging Inc. can help identify the most suitable option.
Many machine vision applications require more than standard lighting. Object shape, surface finish, working distance, camera position, production speed, and inspection goals can all create unique lighting challenges. VA Imaging Inc. offers customization options across its machine vision lighting series to help meet these requirements.
Custom options may include special sizes, custom colors, UV lighting, NIR lighting, specialized wavelengths, application-specific designs, certification-related requirements, single-unit customization, and larger batch customization.
Whether a project requires one custom light or a larger production quantity, VA Imaging Inc. can support application-specific lighting requirements. This flexibility is valuable for system integrators, OEMs, and manufacturers who need lighting that fits the exact mechanical and optical needs of their machine vision setup.
VA Imaging Inc. offers a complete range of machine vision lighting categories designed for different industrial imaging needs. Many series are available in multiple sizes, and several lighting options are available in common colors such as red, blue, green, and white.
Each type of light serves a different purpose. Selecting the right series depends on the inspection task, the object being inspected, the desired contrast, and the camera configuration.
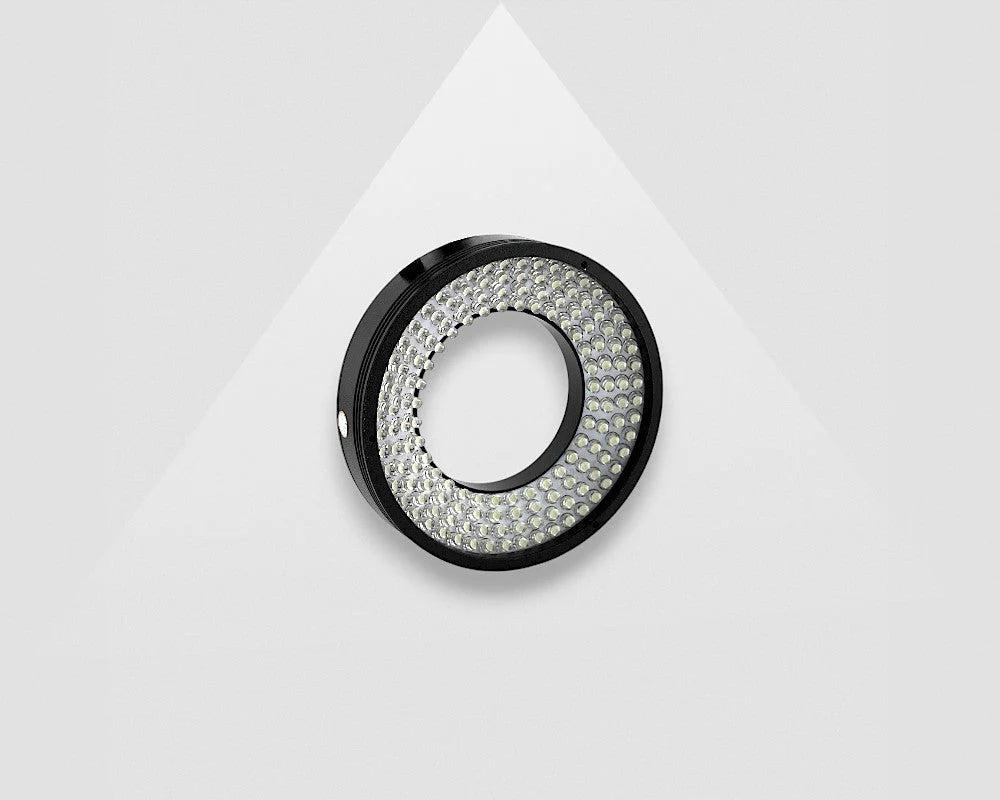
Ring lights are commonly used in machine vision systems that require uniform, shadow-reduced illumination for close-up inspection. Because the light surrounds the camera lens, it can illuminate the object evenly from the viewing direction.
Ring lights are often used for quality control, small-part inspection, automated inspection, surface analysis, and close-range imaging. They are useful when the system needs consistent illumination around the camera’s field of view and when shadows must be reduced during inspection.
VA Imaging Inc. offers multiple ring light options, including standard ring lights, dark field ring lights, diffuse bright field ring lights, and diffuse dark field ring lights. These options help support different inspection needs, from general illumination to applications requiring enhanced contrast or reduced surface glare.
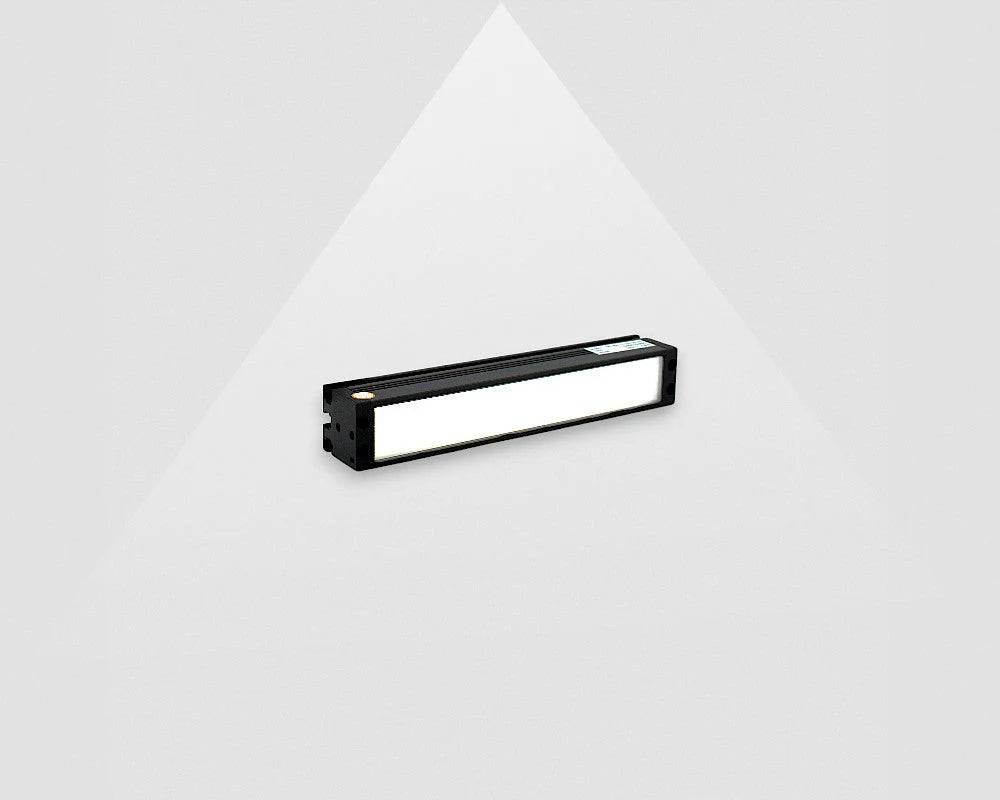
Bar lights are versatile LED Machine vision lights that can be positioned at different angles to control how the object is illuminated. They are often used in pairs to minimize shadows and create even lighting across the inspection area. Because the position is adjustable, bar lights can be mounted close to the object, beside the camera, or at an angle that highlights specific features.
Bar lights are suitable for general machine vision inspection, surface inspection, shape and edge detection, area illumination, shadow reduction, and precision inspection. They are especially useful when the lighting angle needs to be adjusted to match the object surface or inspection target.
For applications where the light must cover a longer working distance or illuminate a larger area, bar lights can provide flexible and reliable Vision System Lighting for many industrial setups.
Coaxial lights are designed for applications where direct, on-axis illumination is required. This lighting approach is useful when precise imaging is needed and reflections or shadows must be reduced.
Coaxial lighting can help reveal details on flat, reflective, or specular surfaces by aligning the light path with the camera’s optical axis. Coaxial lights are commonly used for precision inspection, flat surface imaging, reflective object inspection, fine detail detection, and applications requiring minimal shadows. They are particularly useful when standard angled lighting creates glare or uneven image results.
For machine vision applications involving printed surfaces, flat components, or reflective materials, coaxial lighting can help create a more stable image for automated analysis.

Back lights are used to create a silhouette effect or highlight the outline of an object. Instead of lighting the front surface, the light is placed behind the object, allowing the camera to capture its contour clearly. This is especially useful when the inspection goal is to detect shape, size, position, or separation from the background.
Backlights are often used for object detection, shape recognition, dimensional measurement, contour inspection, part alignment, and silhouette imaging. They are a strong choice when the system needs a clear outline rather than surface detail.
For many US manufacturing applications, backlighting is used to support precise measurement and reliable part detection, especially when consistent contrast is required.

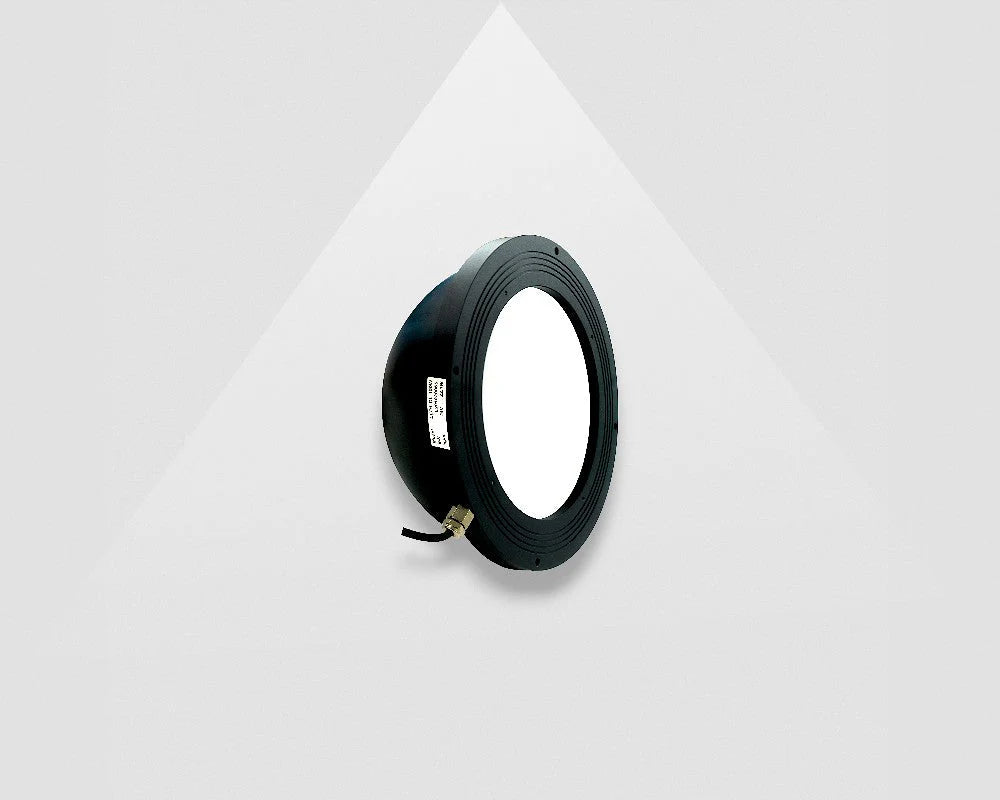
Dome lights provide even, diffuse illumination and are especially useful for reflective, curved, or uneven surfaces. By spreading light across the object from multiple directions, dome lighting helps reduce glare and harsh shadows. This makes it valuable for surface inspection tasks where defects, marks, or fine details must be visible without distortion from reflections.
Dome lights are commonly used for highly reflective objects, surface inspection, defect detection, curved part inspection, and applications requiring soft, even illumination. They are often selected when direct lighting creates hot spots or when the object surface makes inspection difficult.
For applications involving glossy packaging, metal surfaces, rounded parts, or textured components, dome lighting can improve image consistency and inspection reliability.
Line scan lights are designed for machine vision applications involving moving objects, such as products traveling on a conveyor belt. Instead of capturing an entire area at once, line scan imaging captures one line at a time. The lighting must therefore provide intense, consistent illumination across the line being inspected.
Line scan lights are suitable for continuous inspection, conveyor-based imaging, high-resolution inspection, web inspection, surface defect detection, and moving product analysis.
For high-speed inspection environments, line scan lighting is especially important because illumination must remain stable while the object is in motion. Consistent lighting helps the camera capture sequential image data with the accuracy needed for reliable inspection.

Spot lights are among the most commonly used lights in machine vision applications. They are versatile and can be used with industrial cameras in a variety of inspection setups. Spot lights are often useful when inspecting objects with larger fields of view or when controlled directional lighting is required.
Spot lights can be used for camera setups with a wider field of view, flat objects, diffuse objects, general computer vision inspection, and applications requiring adjustable beam angles.
For reflective flat objects, the angle of the LED spot must be adjusted carefully to prevent direct reflections from entering the camera image. For non-flat and non-reflective diffuse objects, LED spot lights can often provide effective illumination.

Machine vision lighting is used across many industries where automated inspection and analysis are required. It helps vision systems capture reliable image data, supporting faster production, better quality control, and more efficient automation.
Common applications include surface inspection, defect detection, high-contrast imaging, object recognition, placement verification, and silhouette creation for part alignment. In manufacturing, machine vision lighting supports inspection on assembly lines by helping detect imperfections, irregularities, dimensional deviations, missing components, and other quality issues.
Machine vision lighting is also widely used in barcode reading and identification tasks. Clear, consistent illumination improves code readability, which helps increase efficiency in logistics, packaging, warehousing, and supply chain operations.
Because automated systems rely on accurate visual data, lighting plays a direct role in improving process stability and reducing inspection errors. As automation continues to advance, Vision System Lighting will remain a key factor in improving industrial efficiency, quality, and production reliability.
Industrial machine vision applications require lighting that remains reliable over long periods of use. Machine vision LED lighting must meet strict requirements for constant light intensity, accurate color rendering, long lifetime, and repeatable performance.
A precise manufacturing process helps ensure these requirements are met. Machine vision lights are designed with a long product life cycle, allowing customers to continue purchasing the same light with the same specifications for many years. This is important for machine builders and manufacturers that need consistency across machines, replacement parts, and long-term production systems.
Batch reproduction is also essential. Minimal LED characteristic variation between production batches helps reduce the risk of quality deviations in vision systems. When lighting output remains consistent, inspection results are more stable and easier to maintain over time.
A dedicated power supply can improve the performance and reliability of a machine vision lighting setup. Instead of relying directly on mains power, a dedicated power supply helps provide consistent illumination, reduce energy consumption, increase reliability, improve control, and minimize electromagnetic interference.
These benefits contribute to the effectiveness and longevity of the overall machine vision system. For many applications, a 24V power supply set is recommended. When the application requires triggering the machine vision lights or controlling intensity, a power supply or light controller may be advised.
The right accessories help ensure that LED Machine vision lights perform consistently and can be properly integrated into the wider automation system.
Selecting the correct machine vision lighting depends on the inspection task and the properties of the object. Important factors include object material, surface texture, reflectivity, shape and size, working distance, camera position, required contrast, inspection speed, measurement accuracy, and available installation space.
A backlight may be best for creating a clear object outline, while a dome light may be better for reflective surfaces. A ring light may work well for close-up inspection, while a line scan light may be required for fast-moving materials on a conveyor. Bar lights offer flexible positioning, and coaxial lights support on-axis imaging for precise inspection of flat surfaces.
For US companies planning new automation systems or improving existing inspection lines, VA Imaging Inc. can help evaluate the lighting requirements and recommend suitable Vision System Lighting solutions.
I am absolutely thrilled with the MER2-160-227U3M camera I purchased from VA-Imaging. The camera exceeds my expectations in every way. The image quality is sharp and clear, even with fast movements. Installation was straightforward. VA-Imaging's customer service was also outstanding. They were very helpful in answering my questions and delivered the camera quickly and securely.
The cameras are a great value for money and the lenses also. The software is outdated and needs refreshing. It took me considerable amount of time to discover how to access the camera features.
Its a pleasure to contact with the sales department. They are very polite and always ready to help. Our orders are always delivered on time and the communication is easy and simple. High quality products.
We initially explored several embedded vision camera and USB3 camera options for our application. Our main priorities were compact dimensions and keeping the required software development to a minimum. We selected a VEN-161 boardlevel camera. It was easy to integrate and USB3 Vision interface allowed our software team to get started quickly. The sales guy was very helpful with selecting the hardware for us. We are happy that we selected the USB3 board-level camera instead of a Mipi embedded vision camera as we didn't require now the additional driver development.
It was easy and quick process from ordering to receiving. One personal message from the team is making it even better. Thanks
In the commercial phase we had maximum support and delivery times were respected. The material is quite good with low and competitive costs.
Most common questions are already answered on our FAQ page. Questions about delivery times, warranty, loan, returns, longevity, manuals etc.
Image processing software captures the images from an industrial camera and performs complex image processing tasks like segmentation, detection, code and text reading.
We share our machine vision knowledge in our knowledge center. Find tutorials how to connect cameras, install software & program I/O.
Check how our customers use our industrial cameras, lenses and lighting in their application
Ask our machine vision experts! We answer rapidly and think along with your imaging project.
The download page provides access to product documentation, software, drivers, manuals and technical resources for industrial cameras and machine vision components.